

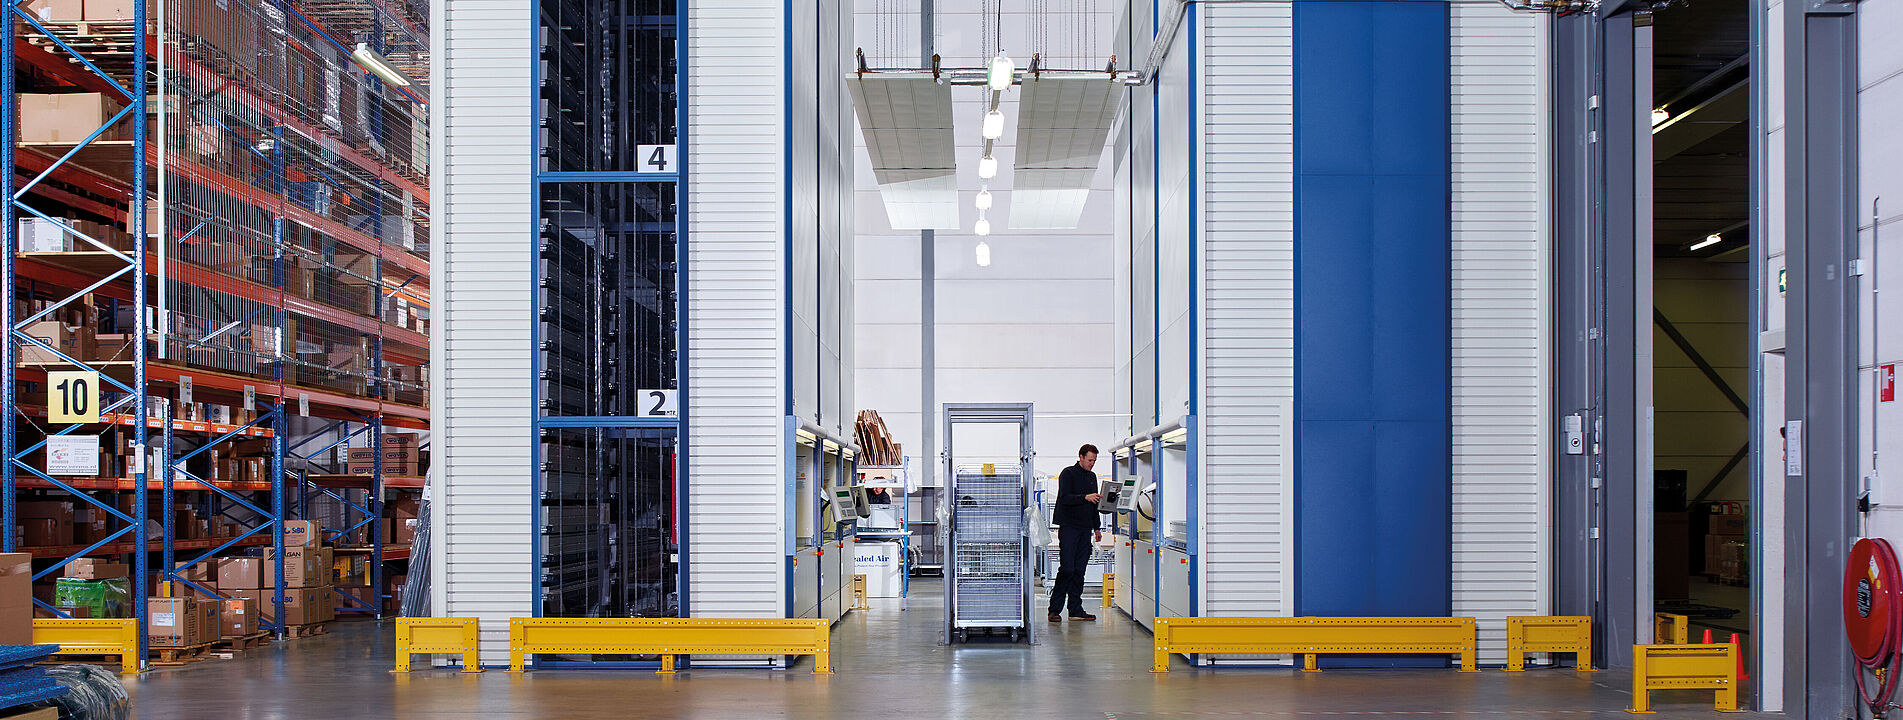
Pallet rack
What is a pallet rack?
A pallet rack is a storage system that holds goods on standardized pallets, stacked on several levels above one another.
The construction behind it is simple: upright frames carry the weight, while horizontal beams support the pallet. That simplicity helps explain why pallet racks are found in nearly every warehouse and distribution center. In many facilities, warehouse pallet racks form the foundation of daily storage operations.
The levels adjust to pallet height, allowing pallet rack shelving to use space more efficiently than floor storage. While traditional pallets stored on the ground typically stop at two or three levels, industrial pallet racks can extend close to the ceiling. Loading and unloading is usually handled by forklift. Warehouse pallet racks remain popular because they combine vertical storage with direct access
Direct access to every pallet, and the ability to expand when needed are among the strongest advantages of pallet storage racking systems. Forklifts require wide aisles, taking up room for more storage. Even so, industrial pallet racks remain one of the most common racking systems in warehouses. Today automated pallet racking continues to balance accessibility, flexibility, and storage capacity.
What types of pallet racks are there?
The type of goods being stored, how often they need to be accessed, and the available floor space all influence the best industrial pallet rack system. In most warehouses, four pallet rack types are commonly used. Most warehouses use a selective pallet racking system. Every pallet position can be reached directly by forklift, allowing different products to be stored side by side without a fixed sequence. This makes them well suited for changing inventories and broad product ranges.
Pallet flow racks work differently. Pallets move through the rack on rollers or inclined lanes, entering from one side and exiting from the other. High-volume operations often prefer this first-in, first-out (FIFO) arrangement because it supports a continuous flow of goods. Mobile racking places rack rows on rails. The rows can be pushed together when an aisle is not needed and opened only where access is required. The result is greater industrial racking storage density because less floor space is dedicated to aisles.
Automation is also becoming more common. Traditional pallet rack systems remain in place, while automated controls and digital warehouse racking systems are added around them to improve efficiency and inventory management.
We look forward to advising you on all aspects of pallet racking!


Automated pallet racks – how modern storage technology works
In an automated pallet rack system, goods movement no longer depends entirely on manual forklift travel. Automated storage solutions, conveyor technology, and control systems perform part of the storage and retrieval process.
The benefits are practical: faster inventory access, fewer manual transports, and goods that are available where the next process requires them. In operations with large inventories and repetitive workflows, these improvements can significantly increase efficiency. Storage and retrieval errors are reduced, and inventory remains traceable because every movement is digitally recorded.
These systems are typically connected to ERP and warehouse management software. Warehouse racking technology reports inventory locations, movements, and transactions into a centralized system, creating greater visibility across warehouse operations. Automation does not replace warehouse processes. It supports them and makes them easier to manage.
Advantages of a pallet rack in daily warehouse operation
Organization is one of the primary advantages of pallet racking. Every pallet position has a defined location, making inventory easier to identify, manage, and track than in block storage.
Space utilization is another benefit. Pallet storage racks build upward, allowing warehouses to increase capacity without expanding their footprint.
Efficiency follows from that organization. Products are stored where the system indicates they should be, helping support faster retrieval and smoother material flow. Defined load capacities, organized storage locations, and improved product protection create a more predictable warehouse environment.
Request our product brochures now!


Heavy duty pallet rack – when weight becomes a factor
Machine parts, metal components, and heavy assemblies can exceed the limits of standard industrial pallet racking. Heavy duty pallet racks are designed to handle these higher load requirements. The system allows products to remain on the same pallet throughout receiving, storage, and retrieval. No transferring or repacking is required, reducing handling time and simplifying the storage process. For very heavy goods, that efficiency can make a significant difference. However, the system must be properly specified. Load capacity, pallet rack dimensions, and material handling requirements should be based on the actual application rather than average catalog ratings.
Hanel Storage Systems – modern solutions for warehouse organization
Warehouse planning continues to evolve as businesses face increasing throughput requirements, limited floor space, and more digital workflows. Hanel develops storage and material staging solutions that help companies improve capacity, accessibility, and inventory control. Traditional pallet racks remain an essential part of many warehouse operations. At the same time, demand for automated storage concepts continues to grow. Hanel systems integrate with existing operations where fast material staging, dense storage, and digital inventory management are priorities.
The Hänel Lean-Lift® and Hänel Rotomat® support efficient material flow and warehouse organization. While floor space savings are often a key consideration, the larger goal is creating a storage strategy that remains reliable and effective for years to come.
Our solutions for pallet racking:

Workshops for the disabled, Upper Palatinate


Get in touch with us now!
Hänel Storage Systems
195 Thorn Hill Road, Suite 100
Warrendale, PA 15086
T +1 (412) 787-3444
E-Mail: info@hanel.us